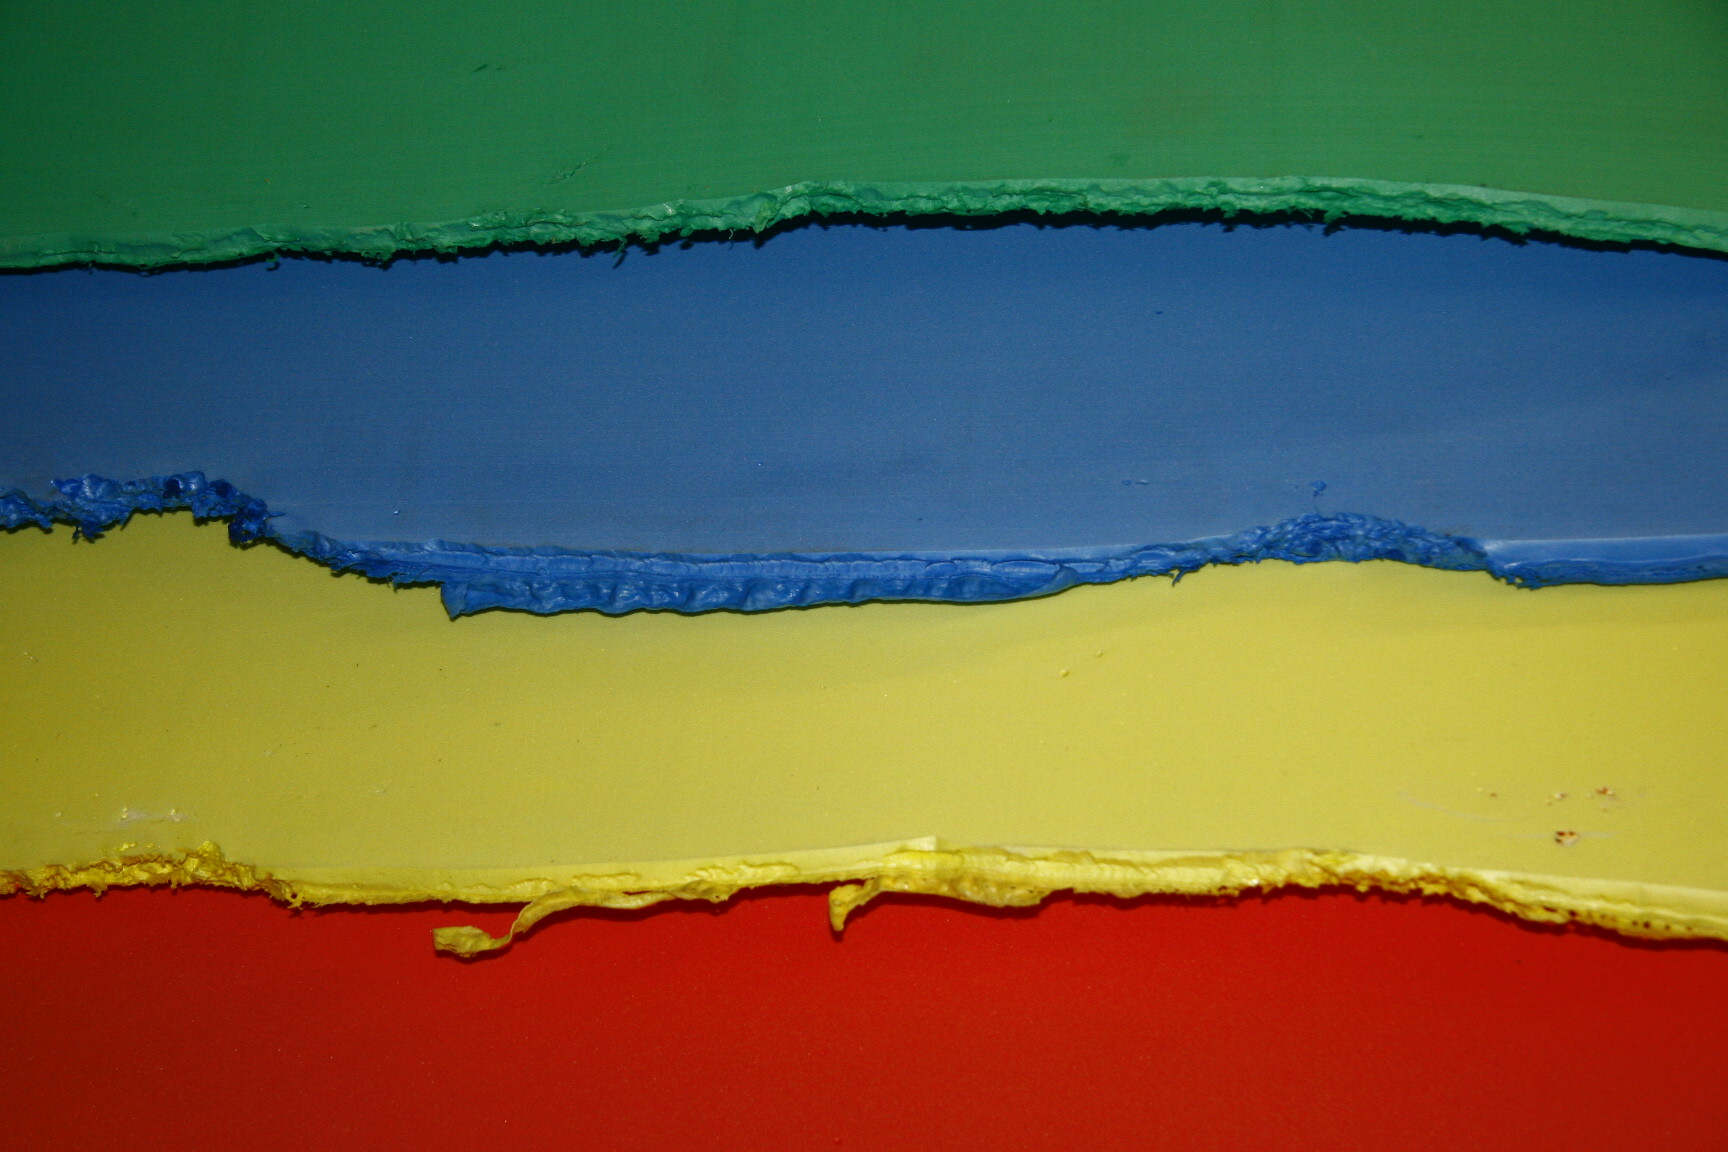
Photo: VYLENCZ. CC BY-SA 4.0 · Original source. Unmodified for this article. The photograph remains under its stated license; no endorsement, specific material grade or JKPD use is implied.

01
Start with polymer, foam and intended function
EVA names an ethylene-vinyl acetate copolymer, not a complete foam specification. Flextech’s EVA technical brief describes closed-cell crosslinked foam, roll and block supply, and heat-forming routes. Use such supplier information together with an identified grade rather than treating the family name as a finished-material guarantee.
For a strap pad, body panel or equipment insert, first decide whether the foam provides contact cushioning, shape or item location. These functions need different evaluations. A description such as high-density EVA does not establish comfort, drop protection or moisture protection. Formulation, cellular structure, thickness and processed condition remain part of the material question.
02
Use the real photograph to discuss supplied form
The photograph above shows coloured foam sheets. The source identifies the material as crosslinked PE or EVA foam; it does not establish a specific polymer grade, density or formulation. Use the image to discuss supplied form, not to identify an EVA grade or a JKPD material.
Label development samples as block, sliced sheet, roll or laminate, and document skin, cut-face and face orientation. Agree where thickness is measured, whether it includes adhesive or textile, and which width and batch are supplied. Record the sample’s intended next process as well. Otherwise two deliveries with the same material-family name may leave very different allowances for forming, cutting or assembly.
03
Density and hardness answer different questions
Apparent density relates mass to volume. Hardness needs a specified indenter, scale and measurement condition. An inquiry stating hardness 45 is incomplete without that context.
Zotefoams’ EV45CN sheet lists apparent density, Shore OO hardness and compression stress separately. These are typical values for one grade, not test results for the illustrated foam or limits for every EVA foam.
Density multiplied by actual volume gives a preliminary foam-mass estimate. This is a calculation, not a measured result. Account separately for cut-outs, holes, textiles and adhesive. Two equal-thickness laminates need not weigh the same, and a heavier candidate is not automatically the more suitable cushioning material.
For a budget calculation only, assume 0.10 square metres of net area, 5 millimetres of foam thickness and density of 45 kilograms per cubic metre. The estimated foam mass is 22.5 grams. These are hypothetical inputs, not a recommended specification or measured sample. If the stated thickness includes a textile face, using the whole thickness overestimates foam volume; ignoring textile mass may then underestimate the complete stack. Calculate layers separately and verify the assembled sample by weighing. This also makes a weight change easier to trace when a supplier alters thickness or lamination.
04
Read compression response and residual deformation separately
The stress needed to reach a stated compression is different from the deformation left after release. The latter must be read with compression level, duration, temperature and recovery time. The Zotefoams sheet separates compression levels and recovery conditions, and states that its typical data do not constitute a supply specification.
Do not treat a quick hand-squeeze as evidence of long-term recovery. Avoid ranking percentages obtained under different conditions. Ask the supplier or laboratory to agree comparable conditions for the intended application. If results are unavailable, record the gap. No density alone supports a claim that padding will never flatten, and a bare recovery number does not explain how a finished strap will feel.
05
Review the processed stack, not only bare foam
Treat die cutting, slicing, heat forming and lamination as identified processing revisions. Retain original sheet, formed parts and assembled stacks to compare thickness at critical locations, edge shape, surface condition and attachment. Obtain temperatures, times and adhesive guidance from the relevant material and equipment suppliers.
A strap specimen should include its actual face textile, mesh, binding and stitching. An insert specimen should include the intended cavity and retrieval clearance. Bare-foam feel does not establish finished-strap comfort. Likewise, closed cells do not establish a waterproof bag: openings, gaps, attachment and load paths still belong to the application review.
06
Keep a process video within its evidence limits
The Flextech video below is supplementary context for foam compression molding. It does not show JKPD manufacturing or identify a process for the illustrated foam. It helps explain why forming route and grade need discussion together; no unverified operating settings are adopted.
For equipment protection, propose evaluation with the intended contents or an explicitly justified equivalent arrangement. Let the project define load, orientation and acceptance criteria. A single press or drop demonstration is not a complete protection claim. Compression data on material specimens also cannot be converted directly into a finished-bag drop rating. Keep material selection, processing approval and product verification as linked but distinct records.
Related video: Compression Molding | Flextech, Inc. · Flextech, Inc.
Supplementary viewing only. This external demonstration is not evidence of the pictured component, certification or finished-bag performance; consult current article-specific documentation.
A demonstration is not performance certification. If the player is unavailable, use the original link; internet access is required.
07
Specify comparable conditions for purchasing
An inquiry should identify function, manufacturer and grade, density and agreed variation, hardness scale, thickness and face condition, supplied form, processing route and the compression and recovery conditions to compare. List adhesive and textile layers separately. Distinguish a target value from an acceptance limit and from a supplier’s typical data.
For substitution, ask whether formulation, foaming, thickness or processing changes before defining the review scope. Retain raw, processed and finished-stack samples with their revisions. That record turns an argument about whether EVA feels hard enough into a specific discussion about which construction meets the project’s stated requirements.
Related reading: Strap padding position and edges.
Share the application, candidate material articles and available records through the JKPD project inquiry page.
Discuss your bag development project
ANSON XIE
General Manager & Founder
Quanzhou Junkai Pengda Special Equipment Co., Ltd.
Email: ansonxie@jkpdtime.com
Phone: +86 177 5095 3355
WhatsApp: +86 177 5095 3355
Factory address: Floors 2–4, Building 1, Phase I, Huixin Intelligent Manufacturing Industrial Park, Hui'an County, Quanzhou, Fujian, China